Unalloyed tantalum UNS R05200 (ASTM B365) | Plain, Twill and Dutch weave | 10–325 mesh, 5–250 µm retention
Technical Datasheet | Tantalum Wire Mesh Series
1. PRODUCT DESCRIPTION
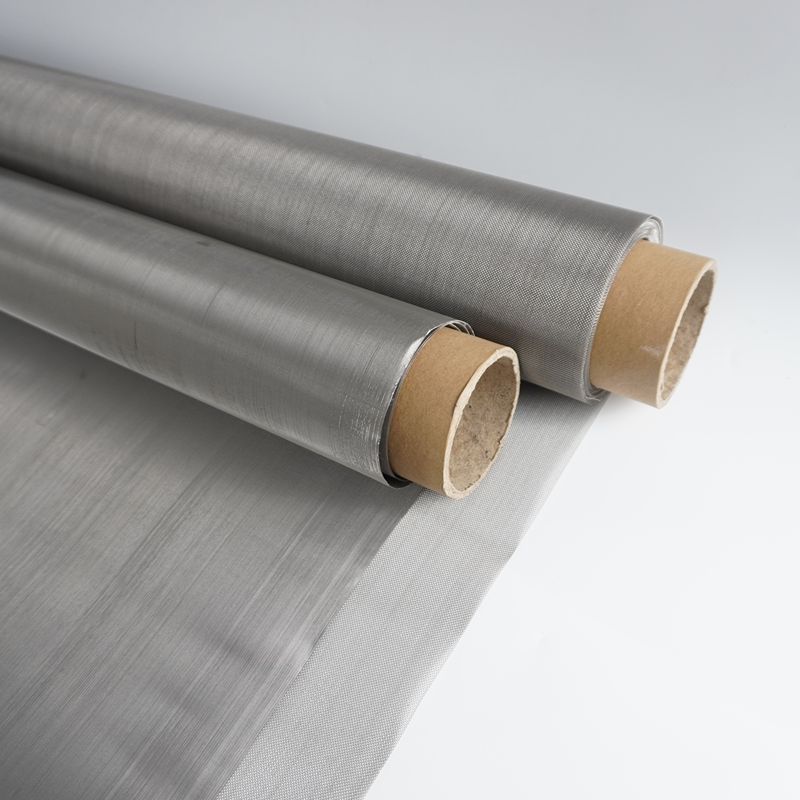
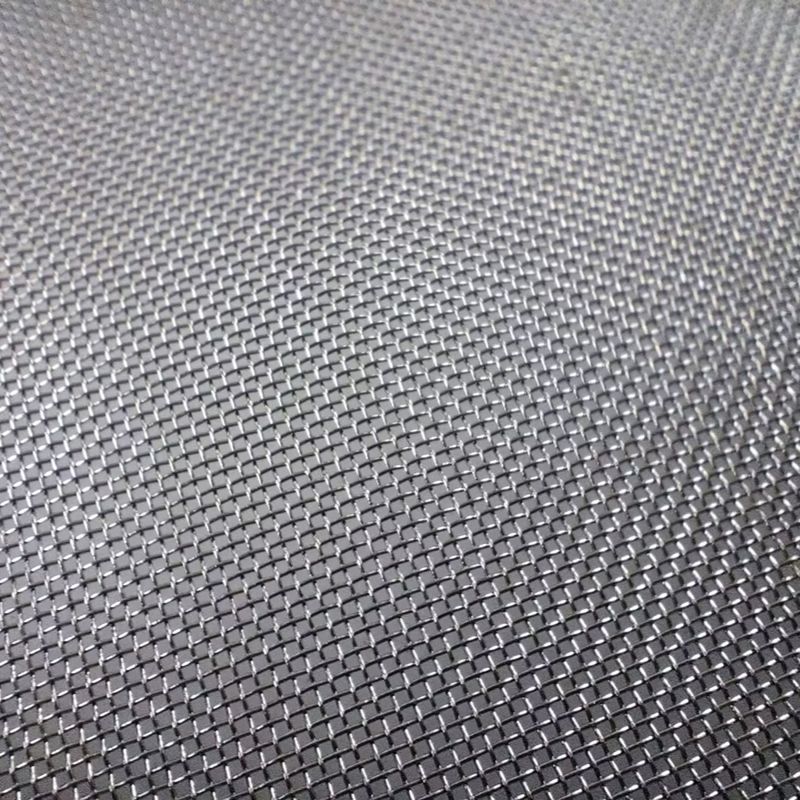
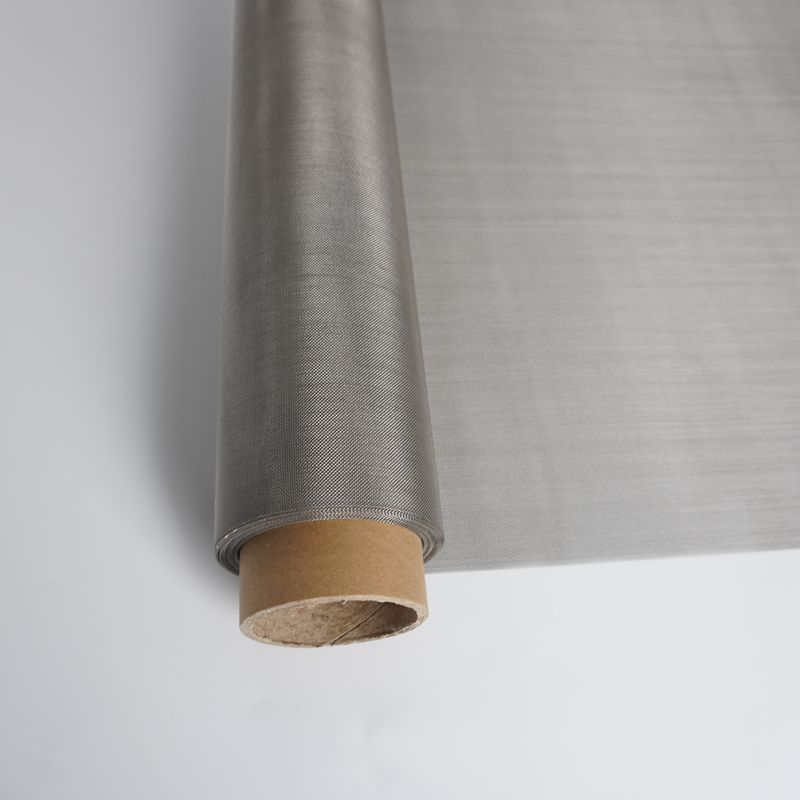
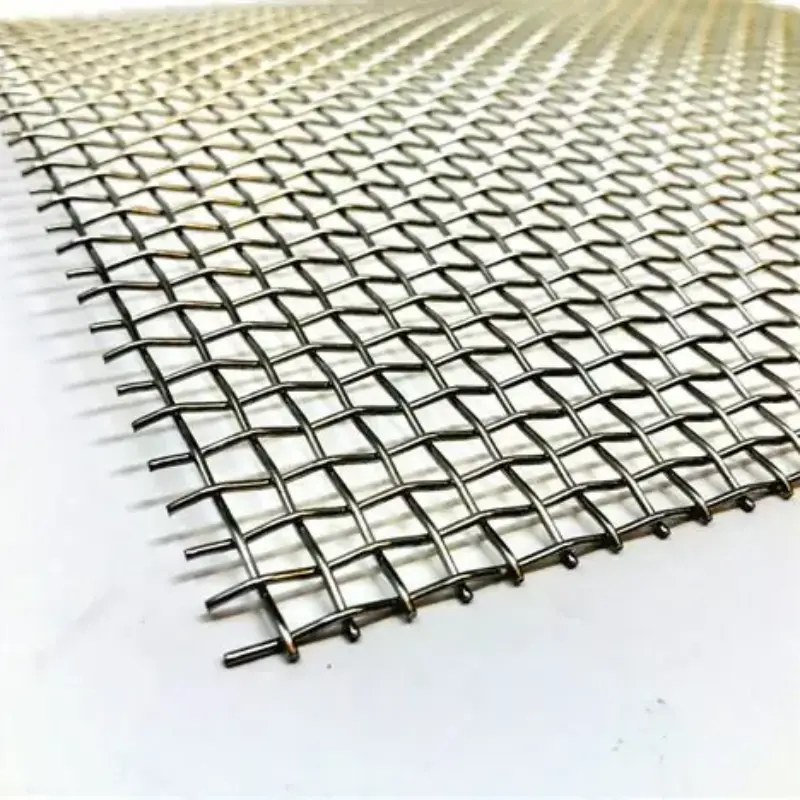
Tantalum wire mesh is a precision woven cloth produced from unalloyed tantalum wire to ASTM B365 / UNS R05200, with a tantalum content of 99.95 % typical against a 99.8 % minimum. Wire is drawn from vacuum-melted ingot, woven on high-tension looms in plain, twill or Dutch construction, then cleaned and annealed. The cloth is supplied flat and dimensionally stable, with square or tapered apertures depending on the weave, and is used as the filtration or support layer in equipment where every other corrosion-resistant metal has already failed.
Tantalum behaves differently from zirconium, titanium and the nickel alloys because its protective film of tantalum pentoxide (Ta₂O₅) is essentially inert in the media that destroy them. Tantalum resists hydrochloric acid, sulphuric acid, nitric acid, phosphoric and organic acids, chlorine and chlorine dioxide, bromine, seawater and even aqua regia, and it remains serviceable at temperatures where titanium and stainless steel are attacked within days. This combination of near-universal acid resistance, a melting point of 2996 °C and outstanding ductility is why tantalum is the reference material for the most aggressive filtration duties in chemical plants, and why it is also specified for medical implants (ASTM F560) and for high-temperature vacuum components.
Tantalum is a dense, expensive metal, so the mesh is normally designed as a thin, high-open-area cloth rather than a heavy screen: the aim is to place the minimum mass of tantalum in the wetted area while keeping enough strength to survive the differential pressure. Standard supply covers 10 to 325 mesh with wire diameters from 0.030 mm to 0.50 mm, widths up to 1.2 m, in rolls, cut panels, discs, cones, pleated packs and welded filter elements. Because of the material value, clean process scrap is recovered and can be credited against future orders under an agreed return-scrap arrangement.
2. MATERIAL OF CONSTRUCTION
Wire is supplied to ASTM B365 (tantalum and tantalum alloy rod and wire) in the annealed condition. Chemical composition and physical properties are summarised below. Tantalum for surgical applications is additionally available to ASTM F560.
| Element |
Requirement (wt. %) |
| Tantalum (Ta) |
99.8 min (99.95 typical) |
| Niobium (Nb) |
0.10 max |
| Tungsten (W) |
0.05 max |
| Molybdenum (Mo) |
0.02 max |
| Oxygen (O) |
0.015 max |
| Carbon (C) |
0.010 max |
| Nitrogen (N) / Iron (Fe) / Nickel (Ni) / Titanium (Ti) |
0.010 max each |
| Silicon (Si) |
0.005 max |
| Hydrogen (H) |
0.0015 max |
Composition according to ASTM B365 for UNS R05200. A mill test certificate to EN 10204 Type 3.1 is issued with every lot; third-party chemical analysis can be arranged on request.
| Physical / Mechanical Property |
Typical Value |
| Density |
16.6 g/cm³ |
| Melting point |
2996 °C |
| Thermal conductivity (20 °C) |
57.5 W/m·K |
| Coefficient of thermal expansion |
6.5 µm/m·K |
| Modulus of elasticity |
≈ 190 GPa |
| Poisson's ratio |
0.34 |
| Specific heat capacity |
140 J/kg·K |
| Tensile strength, annealed |
≈ 210 MPa |
| Yield strength, 0.2% offset, annealed |
≈ 140 MPa |
| Elongation, annealed |
≈ 28 % |
| Magnetic behaviour |
Non-magnetic |
3. WEAVE CONSTRUCTIONS
Four constructions cover the practical range. Selection is driven by the required retention, the allowable pressure drop and the differential pressure across the cloth.
| Construction |
Mesh / inch |
Opening / Rating |
Typical Duty |
| Plain weave |
10–200 |
Coarse to medium screening,
from 2.04 mm down to 77 µm |
General screening, baskets,
support layers |
| Twill weave |
50–325 |
Medium to fine filtration,
from 0.36 mm down to 48 µm |
Fine filters, cartridges,
pleated elements |
| Plain Dutch |
12×64–50×250 |
45–250 µm nominal retention |
Pressure filters, polymer
and acid service |
| Twill Dutch |
20×200–200×1800 |
5–50 µm fine retention |
Fine clarification,
candle and leaf filters |
Plain weave interlaces one wire over one wire and gives identical square apertures in both directions — the most predictable geometry and the easiest cloth to specify. Twill weave passes each wire over two and under two, which supports a finer wire at high counts and produces a stronger, smoother cloth for fine filtration. Dutch weave uses heavy warp wires to carry the load and tightly packed fine weft wires to set the aperture, so a 5 µm rating can be combined with the mechanical strength of a much coarser screen.
4. SPECIFICATIONS — PLAIN WEAVE
Aperture and open area are calculated from wire geometry (aperture = 25.4 / mesh − wire diameter). Weight is calculated from the same geometry at a density of 16.6 g/cm³.
| Mesh / inch |
Wire Dia. (mm) |
Aperture (mm) |
Open Area (%) |
Weight (kg/m²) |
| 10 |
0.500 |
2.040 |
64.5 |
2.57 |
| 20 |
0.400 |
0.870 |
46.9 |
3.28 |
| 30 |
0.300 |
0.547 |
41.7 |
2.77 |
| 40 |
0.250 |
0.385 |
36.8 |
2.57 |
| 50 |
0.200 |
0.308 |
36.8 |
2.05 |
| 60 |
0.190 |
0.233 |
30.4 |
2.22 |
| 80 |
0.130 |
0.188 |
34.9 |
1.39 |
| 100 |
0.100 |
0.154 |
36.8 |
1.03 |
| 150 |
0.065 |
0.104 |
38.0 |
0.65 |
| 200 |
0.050 |
0.077 |
36.8 |
0.51 |
Weight excludes weave crimp; allow +5 to +10 % for woven cloth. Aperture tolerance ±3 %, mesh count ±2 % on standard production; tighter limits on request. Intermediate counts and wire diameters are woven to order.
5. SPECIFICATIONS — TWILL WEAVE
Twill construction is selected between roughly 50 and 325 mesh, where plain weave can no longer carry a practical wire diameter at the required aperture.
| Mesh / inch |
Wire Dia. (mm) |
Aperture (mm) |
Open Area (%) |
Weight (kg/m²) |
| 50 |
0.150 |
0.358 |
49.7 |
1.15 |
| 80 |
0.120 |
0.198 |
38.7 |
1.18 |
| 100 |
0.100 |
0.154 |
36.8 |
1.03 |
| 150 |
0.063 |
0.106 |
39.4 |
0.61 |
| 200 |
0.053 |
0.074 |
34.0 |
0.58 |
| 250 |
0.040 |
0.062 |
36.8 |
0.41 |
| 300 |
0.035 |
0.050 |
34.4 |
0.38 |
| 325 |
0.030 |
0.048 |
38.0 |
0.30 |
Weight excludes crimp; allow +5 to +10 %. Aperture tolerance ±3 % standard, ±1.5 % on request for critical filtration duty.
6. SPECIFICATIONS — DUTCH WEAVE
Rows 1–8 are plain Dutch weave for general purpose filtration; rows 9–14 are twill Dutch weave for fine retention. Warp wires carry the mechanical load, weft wires define the aperture.
| Warp × Weft (per inch) |
Wire Dia. (mm) Warp / Weft |
Nominal Rating (µm) |
Weight (kg/m²) |
| 12 × 64 |
0.58 / 0.40 |
250 |
7.33 |
| 14 × 88 |
0.50 / 0.33 |
180 |
6.72 |
| 16 × 100 |
0.45 / 0.28 |
150 |
5.69 |
| 20 × 110 |
0.40 / 0.25 |
125 |
5.17 |
| 24 × 110 |
0.35 / 0.25 |
100 |
5.04 |
| 30 × 150 |
0.30 / 0.20 |
80 |
4.47 |
| 40 × 200 |
0.25 / 0.15 |
60 |
3.59 |
| 50 × 250 |
0.20 / 0.12 |
45 |
2.87 |
| 20 × 200 |
0.30 / 0.15 |
50 |
3.23 |
| 40 × 560 |
0.20 / 0.08 |
30 |
2.66 |
| 80 × 700 |
0.16 / 0.06 |
20 |
2.48 |
| 120 × 1000 |
0.12 / 0.05 |
15 |
2.17 |
| 165 × 1400 |
0.10 / 0.05 |
10 |
2.64 |
| 200 × 1800 |
0.08 / 0.04 |
5 |
2.14 |
Nominal ratings are reference values, confirmed by bubble-point or glass-bead challenge test on request. Weight excludes crimp; allow +5 to +10 %.
7. KEY FEATURES
▪
Near-universal acid resistance. Tantalum withstands hydrochloric, sulphuric, nitric, phosphoric and organic acids, chlorine, bromine and aqua regia — media in which titanium, zirconium and the nickel alloys are rapidly attacked.
▪
Fine mesh with real ductility. Even at 325 mesh the cloth remains ductile enough to be sheared, rolled, pleated and welded without cracking, so fine filtration no longer means fragile elements.
▪
High-temperature capability. With a melting point of 2996 °C, tantalum mesh serves in vacuum and inert-atmosphere furnaces and in high-temperature process streams far beyond the range of stainless steels.
▪
Thin gauge, high open area. Because the material is expensive, cloth is normally optimised to a thin wire with high open area, keeping wetted mass and pressure drop low.
▪
Biocompatible. Tantalum is accepted for implant applications under ASTM F560, with no reported systemic reaction and excellent soft-tissue response.
▪
Non-magnetic and high density. Non-magnetic in service, with a density of 16.6 g/cm³ that also makes the cloth useful for radiation attenuation and mass-critical components.
▪
Full traceability. Heat number, mill certificate to EN 10204 3.1 and dimensional report accompany every roll, supporting pressure-equipment and medical quality programmes.
8. APPLICATION FIELDS
▪
Chemical processing. Filter elements, catalyst baskets and support screens in hydrochloric, sulphuric and nitric acid plants; heat-exchanger inlet screens; column packing retainers; concentrator and acid-regeneration circuits.
▪
Chlor-alkali and chlorine handling. Chlorine, chlorine dioxide and hypochlorite service, where titanium ignites and stainless steel pits.
▪
Pharmaceutical and fine chemicals. Product-contact filtration and catalyst recovery where no metal ion may leach into the batch.
▪
Polymer and fibre production. Spin-pack and screen-pack filtration of aggressive polymer melts at high temperature and pressure.
▪
Medical devices. Cranial and reconstructive meshes, implant components and surgical filtration hardware, supplied to ASTM F560 on request.
▪
Electronics and sputtering. High-purity filtration of etchants and solvents, sputter-target backing and shielding components in semiconductor and capacitor manufacture.
▪
Aerospace, vacuum and nuclear. High-temperature furnace liners, vacuum system screens, radiation-shielding components and corrosion-resistant assemblies in aggressive coolant or sampling loops.
▪
Marine and offshore. Seawater intake screens and brine-side strainers where chloride attack and biofouling rule out other metals.
9. ADVANTAGES
▪
Equipment life measured in campaigns, not months. In hot hydrochloric and sulphuric acid duty tantalum mesh outlasts stainless steel and titanium by a wide margin, removing repeated screen replacement from the maintenance budget.
▪
Closest inertness to platinum at far lower cost. Tantalum delivers platinum-group corrosion performance at a fraction of the metal price, which is why it replaces platinum and gold in many filter and liner duties.
▪
No contamination of the product. No colouring, catalytic or ionic release into the process stream, protecting batch certification in pharmaceutical and electronic-grade production.
▪
Design margin under pressure. The cloth tolerates high differential pressure even at fine ratings, so elements can be made smaller and fewer for the same duty.
▪
Low wetted mass per unit area. Thin wire and high open area keep the tantalum content — and therefore the capital cost — as low as the duty allows.
▪
Recoverable value. Tantalum retains a high residual value; clean process scrap and end-of-life elements can be returned for credit, partially offsetting the initial purchase.
▪
Certified and repeatable. Every lot is delivered with a 3.1 mill certificate and dimensional report, so repeat orders reproduce the same aperture, weight and filtration rating.
10. SERVICE LIMITS
Tantalum is not universal, and specifying it outside its envelope is the most common cause of premature failure. The following conditions must be reviewed before quotation:
▪
Hydrofluoric acid and fluorides. Tantalum is attacked rapidly by HF and by fluoride-containing media, including some pickling and etching baths.
▪
Fuming sulphuric acid (oleum). Oleum attacks tantalum; the resistance claimed for sulphuric acid applies to the non-fuming grade.
▪
Hot concentrated alkalis. Strong sodium and potassium hydroxide at elevated temperature cause attack; alkaline duty should be confirmed case by case.
▪
Hydrogen and oxygen at temperature. Above roughly 300 °C tantalum absorbs hydrogen and oxygen, which embrittles the wire; high-temperature service should be in vacuum or inert gas, and cathodic protection must be avoided.
▪
Fluorine and strong oxidisers. Elemental fluorine and some powerful oxidisers are outside the recommended envelope.
Actual corrosion rates depend on concentration, temperature, aeration and the presence of chlorides or fluorides. Please supply the full duty conditions with your enquiry and we will confirm the recommended construction — or advise where zirconium, titanium or a nickel alloy is the better economic choice.
11. QUALITY ASSURANCE AND PACKING
Every roll is inspected for mesh count, aperture, wire diameter, width, length and unit weight, and the results are recorded on the inspection report issued with the material certificate. Chemical composition is verified against the mill certificate, and bubble-point or glass-bead challenge testing can be supplied against an agreed acceptance value for critical filtration duty. Third-party inspection (SGS, BV, TUV) is available on request.
Cloth is wound on a rigid core, interleaved with neutral paper, sealed in VCI film and packed in a plywood case or on a pallet with edge protection. Panels travel flat between boards to prevent creasing. Each package is marked with the heat number, mesh count, rating and roll length, and clean process scrap can be segregated and returned under an agreed credit arrangement.